Methylcobalamin Chemical Powder About
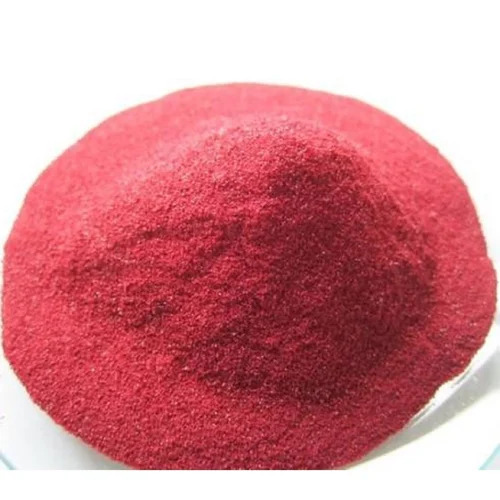
Highlighted as an extraordinary nutritional supplement, Methylcobalamin Chemical Powder is in demand for its first-class quality and high purity. This uncommon formulation is presented as a fine, deep red powder-100% API methylcobalamin-making it the preferred choice for pharma-grade applications. With high bioavailability and light-sensitive stability, it must be handled with care. Last chance to secure this allergen-free, tasteless, odorless vitamin B12 variant for capsules, tablets, and other forms. Supplied in sealed containers, its non-poisonous, highly stable properties guarantee optimal results for distributors, suppliers, and manufacturers.
Versatile Applications and Advanced Features
Methylcobalamin Chemical Powder finds application in a variety of media, most notably in pharmaceutical capsules and tablets as a nutritional supplement. Its high bioavailability supports rapid absorption, ensuring maximum health benefits. The fine powdered form allows seamless blending into formulas, while its neutral pH and water solubility facilitate easy administration. Used at the site of oral medication manufacturing, it is favored by machine fillers due to its consistent particle size and stable compound nature.
Market Presence and Seamless Transactions
Our Methylcobalamin Chemical Powder enjoys a prominent place in the main domestic market of India and is also offered to major export markets worldwide. All products are packaged securely and dispatched promptly to ensure quality retention on arrival. We offer flexible payment terms to suit your needs as a distributor, importer, or manufacturer. With an efficient supply chain and reliable packaging, your orders are handled professionally from processing to delivery.
FAQ's of Methylcobalamin Chemical Powder:
Q: How is Methylcobalamin Chemical Powder typically administered?
A: This product is commonly administered orally, blended into capsules, tablets, or other nutritional supplement forms to enhance vitamin B12 intake.
Q: What are the key benefits of using pharmaceutical grade Methylcobalamin?
A: Pharma grade Methylcobalamin offers high purity, superior bioavailability, and non-poisonous, allergen-free properties, ensuring reliable and effective supplementation.
Q: When should the Methylcobalamin powder be stored and handled with extra care?
A: Due to its light-sensitive and stable nature, it should always be stored in a cool, dry place within its sealed container, away from direct light, to preserve potency.
Q: Where can this fine red powder be used?
A: It is ideal for use in the pharmaceutical industry-especially for the manufacture of capsules, tablets, and other nutritional products requiring stable and effective vitamin B12.
Q: What is the recommended process for dispensing and packaging the powder?
A: The powder is best dispensed using automated machines capable of handling fine, water-soluble powders. Products are packaged in sealed containers to maintain every batch's integrity and freshness.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
